# Molecular Symbol: He
# Molecular Weight: 4.003
# Boiling Point @ 1 atm: -452.1°F (-268.9°C, 4oK)
# Freezing Point @ 367 psia: -459.7°F (-272.2°C, 0oK)
# Critical Temperature: -450.3°F (-268.0°C)
# Critical Pressure 33.0 psia: (2.26 atm)
# Density, Liquid @ B.P., 1 atm: 7.798 lb./cu.ft.
# Density, Gas @ 32°F (0°C), 1 atm: 0.0103 lb./cu.ft.
# Specific Gravity, Gas (Air = 1) @ 32°F (0°C), 1 atm: 0.138
# Specific c Gravity, Liquid @ B.P., 1 atm: 0.125
# Specific c Volume @ 32°F (0°C), 1 atm: 89.77 cu.ft./lb.
# Specific c Volume @ 68°F (20°C), 1 atm: 96.67 cu.ft./lb.
# Latent Heat of Vaporization: 34.9 Btu/lb. mole
# Expansion Ratio, Liquid to Gas, B.P. to 32°F (0°C): 1 to 754
Sunday, November 1, 2009


Physical Properties Of NITROGEN
# Molecular Weight: 28.01
# Boiling Point @ 1 atm: -320.5°F (-195.8°C, 77oK)
# Freezing Point @ 1 atm: -346.0°F (-210.0°C, 63oK)
# Critical Temperature: -232.5°F (-146.9°C)
# Critical Pressure: 492.3 psia (33.5 atm)
# Density, Liquid @ BP, 1 atm: 50.45 lb/scf
# Density, Gas @ 68°F (20°C), 1 atm: 0.0725 lb/scf
# Specific Gravity, Gas (air=1) @ 68°F (20°C), 1 atm: 0.967
# Specific Gravity, Liquid (water=1) @ 68°F (20°C), 1 atm: 0.808
# Specific Volume @ 68°F (20°C), 1 atm: 13.80 scf/lb
# Latent Heat of Vaporization: 2399 BTU/lb mole
# Expansion Ratio, Liquid to Gas, BP to 68°F (20°C): 1 to 694
# Boiling Point @ 1 atm: -320.5°F (-195.8°C, 77oK)
# Freezing Point @ 1 atm: -346.0°F (-210.0°C, 63oK)
# Critical Temperature: -232.5°F (-146.9°C)
# Critical Pressure: 492.3 psia (33.5 atm)
# Density, Liquid @ BP, 1 atm: 50.45 lb/scf
# Density, Gas @ 68°F (20°C), 1 atm: 0.0725 lb/scf
# Specific Gravity, Gas (air=1) @ 68°F (20°C), 1 atm: 0.967
# Specific Gravity, Liquid (water=1) @ 68°F (20°C), 1 atm: 0.808
# Specific Volume @ 68°F (20°C), 1 atm: 13.80 scf/lb
# Latent Heat of Vaporization: 2399 BTU/lb mole
# Expansion Ratio, Liquid to Gas, BP to 68°F (20°C): 1 to 694
Physical Properties Of ARGON
# Molecular Weight: 39.95
# Boiling Point @ 1 atm: -302.6°F (-185.9°C, 87oK)
# Freezing Point @ 1 atm: -308.8°F (-189.4°C, 85oK )
# Critical Temperature: -188.4°F (-122.4°C)
# Critical Pressure: 705.8 psia (48.0 atm)
# Density, Liquid @ BP, 1 atm: 87.40 lb/scf
# Density, Gas @ 68°F (20°C), 1 atm: 0.1034 lb/scf
# Specific Gravity, Gas (air=1) @ 68°F (20°C), 1 atm: 1.38
# Specific Gravity, Liquid (water=1) @ 68°F (20°C), 1 atm: 1.40
# Specific Volume @ 68°F (20°C), 1 atm: 9.67 scf/lb
# Latent Heat of Vaporization: 2804 BTU/lb mole
# Expansion Ratio, Liquid to Gas, BP to 68°F (20°C): 1 to 840
Source
# Boiling Point @ 1 atm: -302.6°F (-185.9°C, 87oK)
# Freezing Point @ 1 atm: -308.8°F (-189.4°C, 85oK )
# Critical Temperature: -188.4°F (-122.4°C)
# Critical Pressure: 705.8 psia (48.0 atm)
# Density, Liquid @ BP, 1 atm: 87.40 lb/scf
# Density, Gas @ 68°F (20°C), 1 atm: 0.1034 lb/scf
# Specific Gravity, Gas (air=1) @ 68°F (20°C), 1 atm: 1.38
# Specific Gravity, Liquid (water=1) @ 68°F (20°C), 1 atm: 1.40
# Specific Volume @ 68°F (20°C), 1 atm: 9.67 scf/lb
# Latent Heat of Vaporization: 2804 BTU/lb mole
# Expansion Ratio, Liquid to Gas, BP to 68°F (20°C): 1 to 840
Source
Saturday, September 12, 2009
Boiling & Freezing Temperature of Components in Natural Gas
Natural gas contains component such as Methane, Ethane, Propone, and other inert gas. Following table list the Boiling and Freezing temperature at ATM which is sometime useful.
| COMPONENT | Abbr. | Boiling Temperature (degC) | Freezing Temperature (degC) |
| Helium | He | - 268.6 | |
| Hydrogen | H2 | - 252.5 | |
| Nitrogen | N2 | - 195.8 | - 209.9 |
| Methane | C1 | - 164.0 | |
| Carbon Dioxide | CO2 | - 78.5 | |
| Freon 12 | Freon-12 | - 29.8 | |
| Water | H2O | 0.0 |
Other Interesting Article
- HC Gas Heat capacity ratio (Approx.)
- Conversion from Weight Fraction to Mole Fraction
- Unit Conversion in Energy in LNG Sector
- Wobbe Index
Saturday, August 29, 2009
Flammability Limits
Flammability Limits
Lower flammable limit (LFL) or Lower Explosive Limit (LEL) is minimum vapor concentration in air which a mixture will burn when an ignition source is present.
Upper flammable limit (UFL) or Upper Explosive Limit (UEL) is maximum vapor concentration in air which a mixture will burn when an ignition source is present.
LFL/LEL and UFL/UEL for some common gases are indicated in table below. Some of the gases are commonly used as fuel in combustion processes.
Lower flammable limit (LFL) or Lower Explosive Limit (LEL) is minimum vapor concentration in air which a mixture will burn when an ignition source is present.
Upper flammable limit (UFL) or Upper Explosive Limit (UEL) is maximum vapor concentration in air which a mixture will burn when an ignition source is present.
Concentration of mixture of vapor in air below LFL/LEL (too lean) or above UFL/UEL (too rich), mixture will not burn even an ignition source is present. Therefore, flammable range or explosive range is concentrations between LFL/UFL and UFL/UEL.
LFL/LEL and UFL/UEL for some common gases are indicated in table below. Some of the gases are commonly used as fuel in combustion processes.
| Fuel Gas | (LFL/LEL) (%) | (UEL/UFL) (%) |
| Acetaldehyde | 4 | 60 |
| Acetone | 2.6 | 12.8 |
| Acetylene | 2.5 | 81 |
| Ammonia | 15 | 28 |
| Arsine | 5.1 | 78 |
| Benzene | 1.35 | 6.65 |
| n-Butane | 1.86 | 8.41 |
| iso-Butane | 1.80 | 8.44 |
| iso-Butene | 1.8 | 9.0 |
| Butylene | 1.98 | 9.65 |
| Carbon Disulfide | 1.3 | 50 |
| Carbon Monoxide | 12 | 75 |
| Cyclohexane | 1.3 | 8 |
| Cyclopropane | 2.4 | 10.4 |
| Dimethyl Ether | 3.4 | 27 |
| Diethyl Ether | 1.9 | 36 |
| Ethane | 3 | 12.4 |
| Ethylene | 2.75 | 28.6 |
| Ethylene Oxide | 3.6 | 100 |
| Ethyl Alcohol | 3.3 | 19 |
| Ethyl Chloride | 3.8 | 15.4 |
| Fuel Oil No.1 | 0.7 | 5 |
| Hydrogen | 4 | 75 |
| Isobutane | 1.8 | 9.6 |
| Isopropyl Alcohol | 2 | 12 |
| Gasoline | 1.4 | 7.6 |
| Kerosine | 0.7 | 5 |
| Methane | 5 | 15 |
| Methyl Alcohol | 6.7 | 36 |
| Methyl Chloride | 10.7 | 17.4 |
| Methyl Ethyl Ketone | 1.8 | 10 |
| Naphthalene | 0.9 | 5.9 |
| n-Heptane | 1.0 | 6.0 |
| n-Hexane | 1.25 | 7.0 |
| n-Pentene | 1.65 | 7.7 |
| Neopentane | 1.38 | 7.22 |
| Neohexane | 1.19 | 7.58 |
| n-Octane | 0.95 | 3.20 |
| iso-Octane | 0.79 | 5.94 |
| n-Pentane | 1.4 | 7.8 |
| iso-Pentane | 1.32 | 9.16 |
| Propane | 2.1 | 10.1 |
| Propylene | 2.0 | 11.1 |
| Silane | 1.5 | 98 |
| Styrene | 1.1 | 6.1 |
| Toluene | 1.27 | 6.75 |
| Triptane | 1.08 | 6.69 |
| p-Xylene | 1.0 | 6.0 |
Note : The limits indicated are for component and air at 20oC and atmospheric pressure.
Others Interesting Articles
Friday, August 28, 2009
Minimum Oxygen Concentration (MOC)
Standard air composition is the bulk average air composition encountered at or around sea level. Typically it contains the following composition.
| Component | Abbr. | %Wt | %Vol. | MW |
| Nitrogen | N2 | 75.47 | 78.08 | 28.01 |
| Oxygen | O2 | 23.20 | 20.95 | 32.00 |
| Carbon Dioxide | CO2 | 0.0590 | 0.038 | 44.01 |
| Hydrogen | H2 | 0 | 0.00005 | 2.02 |
| Argon | Ar | 1.28 | 0.93 | 39.95 |
| Neon | Ne | 0.0012 | 0.0018 | 20.18 |
| Helium | He | 0.00007 | 0.0005 | 4.00 |
| Krypton | Kr | 0.0003 | 0.0001 | 83.80 |
| Xenon | Xe | 0.00004 | 8.7x10^-6 | 131.30 |
From standard air composition at sea level, the oxygen content is approximately 20.95% by volume. Oxygen is the main component in fire triangle in generating of fire. From chemistry, without any one of the element, a fire will NOT form.

Although Oxygen is the major component in generating fire, there is still a minimum oxygen concentration (MOC) required present combustible mixture so that a fire can be initiated. Below this limit, a fire will not form. Base on this principle, hydrocarbon mixture is purge with inert gas such as Nitrogen, Carbon dioxide, etc so that the MOC is not reach and therefore combustible mixture is not form.

Common unit used for MOC is % oxygen in air plus fuel. Following table listed several
| Component | MOC (%O2) |
| Hydrogen | 4.0 |
| Acetylene | 6.2 |
| Methane (C1) | 12 |
| Ethane (C2) | 11.2 |
| Ethylene (C2=) | 9.9 |
| Propane (C3) | 11.6 |
| Propylene (C3=) | 11.5 |
| Butane (C4) | 12.3 |
| 1-Butene (C4=) | 11.0 |
| Pentane (C5) | 11.8 |
| Hexane (C6) | 11.8 |
| Benzene | 11.5 |
| Methyl Alcohol | 9.9 |
| Ethyl Alcohol | 10.5 |
| Dimethyl Ether | 10.5 |
| Diethyl Ether | 10.2 |
| Methyl Acetate | 11.0 |
| Methyl Ether Ketone | 11.0 |
| Carbon Disulfide | 5.0 |
Generally a mixtures of Hydrocarbon vapor MOC is around 10% Vol.
API STD 520 recommends MOC of 6 %Vol. for flare stack design to avoid combustible mixture present in flare system. Hydrogen rich flare gas shall consider lower MOC i.e. 3-4% vol.
Ref : "Application of Flammability Diagram For Evaluation of Fire & Explosion Hazards of Flammable Vapor", C.V. Mashuga, D.A. Crowl
Others Interesting Articles
Sunday, August 16, 2009
Conversion from MMSCFD to kg/s
How to convert MMSCFD to Kg/s ?
Standard condition (S) measure at 1.01325 bara & 15.56 degC (60 degF)
Normal condition (N) measure at 1.01325 bara & 0 degC
1.0 MMSCFD
= 1,000,000/(24 x 3600) Sft³ /s
= 1,000,000/(24 x 3600)/35.3152 Sm³/s
= 1,000,000/(24 x 3600)/35.3152 x (273.15/288.71) Nm³/s
= 1,000,000/(24 x 3600)/35.3152 x (273.15/288.71)/22.414 kmol/s
= 1 / 72.2826
Standard condition (S) measure at 1.01325 bara & 15.56 degC (60 degF)
Normal condition (N) measure at 1.01325 bara & 0 degC
1.0 MMSCFD
= 1,000,000/(24 x 3600) Sft³ /s
= 1,000,000/(24 x 3600)/35.3152 Sm³/s
= 1,000,000/(24 x 3600)/35.3152 x (273.15/288.71) Nm³/s
= 1,000,000/(24 x 3600)/35.3152 x (273.15/288.71)/22.414 kmol/s
= 1 / 72.2826
1 MMSCFD = 1 / 72.2826 kmol/s
or
1 MMSCFD = MW / 72.2826 kg/s
MW = Molecular weight
Other Interesting Articles
or
1 kg/s = 72.2826 / MW MMSCFD
MW = Molecular weight
Other Interesting Articles
Saturday, June 20, 2009
Thermal Conductivity & Unit Conversion
Thermal conductivity (k) is ability of heat conduction for material. It is heat (Q) transmitted through a unit thickness (x) in a direction normal to a surface of unit area (A) with temperature difference (dT) at steady state conditions.
Thermal conductivity Unit & Conversion
k = (Q/A).x / dT
Thermal conductivity Unit & Conversion
- 1 W/(mK) = 0.85985 kcal/(hr.moC)
- 1 W/(mK) = 0.57779 Btu/(ft.hr oF)
- 1 W/(mK) = 6.9335 Btu.in/(ft2.hr oF)
| Material | 25oC |
| Acetone | 0.16 |
| Acrylic | 0.2 |
| Air | 0.024 |
| Alcohol | 0.17 |
| Aluminum | 250 |
| Aluminum Oxide | 30 |
| Ammonia | 0.022 |
| Antimony | 18.5 |
| Argon | 0.016 |
| Asbestos-cement board | 0.744 |
| Asbestos-cement sheets | 0.166 |
| Asbestos-cement | 2.07 |
| Asbestos, loosely packed | 0.15 |
| Asbestos mill board | 0.14 |
| Asphalt | 0.75 |
| Balsa | 0.048 |
| Bitumen | 0.17 - 0.33 |
| Benzene | 0.16 |
| Beryllium | 218 |
| Brass | 109 |
| Brick dense | 1.31 |
| Brick work | 0.69 |
| Cadmium | 92 |
| Carbon | 1.7 |
| Carbon dioxide | 0.0146 |
| Carbon Steel | 50 |
| Cement, portland | 0.29 |
| Cement, mortar | 1.73 |
| Chalk | 0.09 |
| Chrome Nickel Steel (18% Cr, 8 % Ni) | 16.3 |
| Clay, dry to moist | 0.15 - 1.8 |
| Clay, saturated | 0.6 - 2.5 |
| Cobalt | 69 |
| Concrete, light | 0.42 |
| Concrete, stone | 1.7 |
| Constantan | 22 |
| Copper | 401 |
| Corian (ceramic filled) | 1.06 |
| Corkboard | 0.043 |
| Cork, regranulated | 0.044 |
| Cork | 0.07 |
| Cotton | 0.03 |
| Cotton Wool insulation | 0.029 |
| Diatomaceous earth (Sil-o-cel) | 0.06 |
| Earth, dry | 1.5 |
| Ether | 0.14 |
| Epoxy | 0.30 - 0.35 |
| Felt insulation | 0.04 |
| Fiberglass | 0.04 |
| Fiber insulating board | 0.048 |
| Fiber hardboard | 0.2 |
| Fireclay brick 500oC | 1.4 |
| Foam glass | 0.045 |
| Freon 12 | 0.073 |
| Gasoline | 0.15 |
| Glass | 1.05 |
| Glass, Pearls, dry | 0.18 |
| Glass, Pearls, saturated | 0.76 |
| Glass, window | 0.96 |
| Glass, wool Insulation | 0.04 |
| Glycerol | 0.28 |
| Gold | 310 |
| Granite | 1.7 - 4.0 |
| Gypsum or plaster board | 0.17 |
| Hairfelt | 0.05 |
| Hardboard high density | 0.15 |
| Hardwoods (oak, maple..) | 0.16 |
| Helium | 0.142 |
| Hydrogen | 0.168 |
| Ice (0oC, 32oF) | 2.18 |
| Insulation materials | 0.035 - 0.16 |
| Iridium | 147 |
| Iron | 80 |
| Iron, wrought | 59 |
| Iron, cast | 55 |
| Kapok insulation | 0.034 |
| Kerosene | 0.15 |
| Lead Pb | 35 |
| Leather, dry | 0.14 |
| Limestone | 1.26 - 1.33 |
| LPG | 0.23 - 0.26 |
| Magnesia insulation (85%) | 0.07 |
| Magnesite | 4.15 |
| Magnesium | 156 |
| Marble | 2.08 - 2.94 |
| Mercury | 8 |
| Methane | 0.030 |
| Methanol | 0.21 |
| Mica | 0.71 |
| Mineral insulation materials, wool blankets .. | 0.04 |
| Mineral oil | 0.138 |
| Molybdenum | 138 |
| Monel | 26 |
| Mud | 1.3 - 2.6 |
| Neoprene Rubber | 0.3 |
| Nickel | 91 |
| Nitrogen | 0.024 |
| Nylon 6 | 0.25 |
| Oil, machine lubricating SAE 50 | 0.15 |
| Olive oil | 0.17 |
| Oxygen | 0.024 |
| Paper | 0.05 |
| Paraffin Wax | 0.25 |
| Perlite, atmospheric pressure | 0.031 |
| Perlite, vacuum | 0.00137 |
| Plaster, gypsum | 0.48 |
| Plaster, metal lath | 0.47 |
| Plaster, wood lath | 0.28 |
| Plastics, foamed (insulation materials) | 0.03 |
| Platinum | 70 |
| Plywood | 0.13 |
| Polyethylene HD | 0.42 - 0.51 |
| Polypropylene | 0.1 - 0.22 |
| Polystyrene expanded | 0.03 |
| Polyurethane | 0.2 |
| Polyurethane Foam (Dry) | 0.02 - 0.04 |
| Polyurethane Foam (Dry) | 0.4 - 0.6 |
| Porcelain | 1.5 |
| PTFE | 0.25 |
| PVC | 0.19 |
| PVC Foam ((Dry) | 0.040 - 0.044 |
| Pyrex glass | 1.005 |
| Quartz mineral | 3 |
| Rock, solid | 2 - 7 |
| Rock, porous volcanic (Tuff) | 0.5 - 2.5 |
| Rock Wool insulation | 0.045 |
| Sand, dry | 0.15 - 0.25 |
| Sand, moist | 0.25 - 2 |
| Sand, saturated | 2 - 4 |
| Sandstone | 1.7 |
| Sawdust | 0.08 |
| Silica aerogel | 0.02 |
| Silicone oil | 0.1 |
| Silver | 429 |
| Snow (temp <>oC) | 0.05 - 0.25 |
| Sodium | 84 |
| Softwoods (fir, pine ..) | 0.12 |
| Soil, with organic matter | 0.15 - 2 |
| Soil, saturated | 0.6 - 4 |
| Steel, Carbon 1% | 43 |
| Stainless Steel | 16 |
| Straw insulation | 0.09 |
| Styrofoam | 0.033 |
| Syntactic Foam (dry) | 0.09 |
| Syntactic Foam (wet) | 0.3 |
| Tin Sn | 67 |
| Zinc Zn | 116 |
| Urethane foam | 0.021 |
| Vermiculite | 0.058 |
| Vinyl ester | 0.25 |
| Water | 0.58 |
| Wood across the grain, white pine | 0.12 |
| Wood across the grain, balsa | 0.055 |
| Wood across the grain, yellow pine | 0.147 |
| Wood | 0.17 |
| Wool | 0.07 |
Ref :
1) Thermal Conductivity - Huskseflux
2) Thermal Conductivity - NDT Resource
3) Thermal Conductivity Conversion Calculator
4) Thermal Conductivity of Metal
5) Soil Thermal Conductivity
6) Misc. on Thermal Conductivity
7) Thermal Conductivity for Various Material
Others Interesting Articles
Sunday, January 11, 2009
Pump Suction Specific Speed (Nss)
Suction specific speed ( Nss) of a pump is a dimensionless number expressed as
Nss=( N* Q 0.5 ) / (NPSHr)0.75
Where
Nss : Suction Specific speedPump manufacturer normally would design a pump with the Suction specific speed (Nss) below 10000 to ensure a healthy life span as high Nss would leads to rough operation and shorten life span. Some manufacturer may design for 8000-8500 .
Q : Flow rate (gpm) at the Best Efficiency Point
N : Pump rotational speed (rpm)
NPSHr : Net Positive Suction Head required (ft)
To achieve lower NPRHr;
- reduce pump speed (N)
- reduce flow i.e. double suction (Q)
- increase Suction Specific Speed (Nss)
Example :
Flow 2,500 gpm, head 800 ft, pump rotational speed 2950 rpm.
What NPSHr will be required?
Nss = ( N* Q 0.5 ) / (NPSHr)0.75
10000 = (2950 * 2500 0.5 ) / (NPSHr)0.75NPSHr = 36.17 ft
Other Interesting Articles
Quick Determination of Steam Saturated Temperature (Tsat)
What is quick estimation of steam saturated temperature ?
Square-root-Square-root formula may be used. The formula is :
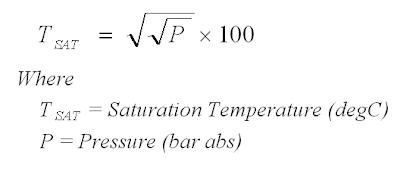
Square-root-Square-root formula may be used. The formula is :
Monday, November 24, 2008
Relief Valve Standard API Effective Orifice Area
Relief Valve Standard API Effective Orifice Area
API has generated the standard API Effective Orifice Area with corresponding designation letter (following table). Besides, standard effective orifice area, it also has a series of corresponding inlet size, outlet size combination for various pressure classes of flanged relief valves. All these information are tabulated in API Std 526 Flanged Steel Pressure Relief Valves.
| API Relief Valve Standard Effective Discharge Orifice Areas | ||
| Designation | in2 | cm2 |
| D | 0.110 | 0.71 |
| E | 0.196 | 1.26 |
| F | 0.307 | 1.98 |
| G | 0.503 | 3.24 |
| H | 0.785 | 5.06 |
| J | 1.287 | 8.30 |
| K | 1.838 | 11.85 |
| L | 2.853 | 18.40 |
| M | 3.600 | 23.23 |
| N | 4.340 | 28.00 |
| P | 6.380 | 41.16 |
| Q | 11.050 | 71.29 |
| R | 16.000 | 103.22 |
| T | 26.000 | 167.74 |
One shall remember above effective areas are valid only when used with the sizing equations contained in API RP 520 Part I - Sizing, Selection & Installation of Pressure-Relieving Devices in Refinery.
Related Articles
- What is Capacity Correction Factor (CCF) due to Back pressure for PSV ?
- PSV Constant Back Pressure Correction Factor (Kb) for Vapor & Gas
- Several Impact of Backpressure on Conventional PRV
- How Back Pressure Affect Conventional PSV Set Pressure Subject to It Vent
- Back Pressure Affect Conventional PSV Set Pressure : Case Study #1 - Bonnect Vent to ATM
- Back Pressure Affect Conventional PSV Set Pressure : Case Study #2 - Non-Bonnect Vent
Tuesday, November 18, 2008
HC Gas Heat capacity ratio (Approx.)
Heat capacity ratio (or Isentropic exponent, k) is the ratio of specific heat capacity at constant pressure (CP) to specific heat capacity at constant volume (CV). It is commonly used in critical pressure ratio estimation, compression head estimation, etc. Following is a approximate k factor of Hydrocarbon gases. It may be used when only HC gas molecular weight (MW) and temperature (T) is available.

Source : GPSA
Other Interesting Article
Typical Efficiency for Compressor
Compressor efficiency is very much subject to compressor type, design, etc. It possibly range from 50% to 90%. Each compressor from different manufacturer may have different efficiency. Following are some typical compressor efficiency may be used during design phase. It shall be decided by compressor manufacturer.
Centrifugal : 75-80%
Note : nowadays several manufacturers may have some compressor efficiency upto 84%.
Centrifugal : 75-85%
Reciprocating :
- 65% with Compression ratio of 1.5
- 75% with Compression ratio of 2.0
- 80-85% with Compression ratio of 3-6
Rotary : 70%
Other Interesting Articles
Saturday, November 1, 2008
Why CO2 with present of water is corrosive ?
Carbon dioxide (chemical formula: CO2 ) is a chemical compound composed of two oxygen atoms covalently bonded to a single carbon atom. It is a gas at standard temperature and pressure and present in oil and gas fluid. CO2 by itself is not corrosive, however, with the present of free water (H2O), it becomes corrosive and poses a thread to many oil and gas facilities.
CO2 with present of free water would lead to generation of Carbonic acid (H2CO3).
When Carbonic Acid contact with steel (Fe), reaction occur.
2Fe + H2CO3 ==> Fe2CO3 + H2
With minimum level of Oxygen would aggregate the corrosion :
Corrosion without Acid Carbonic :
and Corrosion with Acid Carbonic :
Carbonic acid is weak acid would reduce the pH of fluid and this further aggregate the corrosion.
Other Interesting Article
Thursday, October 30, 2008
Relationship Between MOP & MAOP
Maximum Operating Pressure (MOP)
A maximum pressure at any expected normal operating scenario.
Maximum Allowable Operating Pressure (MAOP)
A maximum pressure that allowable by any equipment and device to operate satisfactory without affecting it performance. Example, a conventional direct spring loaded pressure relief valve allow MOP is 90% of set pressure whilst a pilot operated pressure relief valve may allow upto 97-98% of set pressure.
For Design Pressure & MAWP, read in "Relationship Between Design Pressure & Maximum Allowable Working Pressure (MAWP)".
A maximum pressure at any expected normal operating scenario.
Maximum Allowable Operating Pressure (MAOP)
A maximum pressure that allowable by any equipment and device to operate satisfactory without affecting it performance. Example, a conventional direct spring loaded pressure relief valve allow MOP is 90% of set pressure whilst a pilot operated pressure relief valve may allow upto 97-98% of set pressure.
For Design Pressure & MAWP, read in "Relationship Between Design Pressure & Maximum Allowable Working Pressure (MAWP)".
MOP <= MAOP < Design Pressure <= MAWP
Sunday, October 26, 2008
Determine Interstage Pressure for Multi-stages Centrifugal Compressor
How to determine interstage pressure for multi-stages centrifugal compressor ?
For a n-stages centrifugal compressor system with inlet and outlet pressure of P0 and Pn, the compression ratio (r) should be about the same in each stage.
For a n-stages centrifugal compressor system with inlet and outlet pressure of P0 and Pn, the compression ratio (r) should be about the same in each stage.
r = (Pn/P0)(1/n)
P1 = r.P0
P2 = r.P1
P3 = r.P2
.
.
.
Pn = r.Pn-1
P2 = r.P1
P3 = r.P2
.
.
.
Pn = r.Pn-1
Pressure Head Increases for Fan and Blower
What is pressure head increases for a fan and/or a blower ?
Fans are used to increase pressure head by about 3%, 12" water (300mm H2O)
Blowers are used to increase pressure head to lower than 2.75 barg (40 psig)
Fans are used to increase pressure head by about 3%, 12" water (300mm H2O)
Blowers are used to increase pressure head to lower than 2.75 barg (40 psig)
Monday, October 20, 2008
Relationship Between Design Pressure & Maximum Allowable Working Pressure (MAWP)
Maximum Allowable Working Pressure (MAWP)
Design pressure
Maximum gauge pressure permissible at the top of a completed vessel in its normal operating position at the designated coincident temperature specified for that pressure. MAWP is the least of the values for the internal or external pressure as determined by the vessel design rules for each element of the vessel using actual nominal thickness, exclusive of additional metal thickness allowed for corrosion and loadings other than pressure. The MAWP is the basis for the pressure setting of the pressure-relief devices that protect the vessel.
Design pressure
A pressure with coincident design temperature, used to determine the minimum permissible thickness or physical characteristic of each component, as determined by the design rules of the pressure-design code. The design pressure is selected by the designer to provide a suitable margin above the most severe pressure expected during normal operation at a coincident temperature. The design pressure is equal to or less than the Maximum Allowable Working Pressure (MAWP).
Design Pressure <= MAWP
Note :
Design pressure is normally the Pressure Relief Valve (RV) set pressure of a vessel. This pressure at coincident temperature is used to determine the minimum wall thickness. A calculated thickness is 9 mm based on a design pressure @ coincident temperature. However, with a standard material thickness of 10 mm. The MAWP would be calculated pressure based on this thickness.
Design pressure is normally the Pressure Relief Valve (RV) set pressure of a vessel. This pressure at coincident temperature is used to determine the minimum wall thickness. A calculated thickness is 9 mm based on a design pressure @ coincident temperature. However, with a standard material thickness of 10 mm. The MAWP would be calculated pressure based on this thickness.
Saturday, October 11, 2008
Absolute & Relative Roughness for Piping Material
What is absolute & Relative roughness for piping material ?
* 1m = 1,000 mm = 1,000,000 micron ; 1 mm = 1,000 micron
Pipe Relative roughness
Relative pipe roughness is the ratio of absolute roughness (e) by and pipe diameter (D) :
(1) Binder, R.C. (1973), Fluid Mechanics, Prentice-Hall, Inc. (Englewood Cliffs, NJ).
(2) GPSA & Crane Technical Paper No. 410M
(3) Darby, R. (2001), Fluid Mechanics for Chemical Engineers, Vol 2, Marcel Dekker, (NY)
(4) BP GP 44-80
(5) Fiberglass Pipe Handbook, SPI Composites Institute
(6) Enginereed Software’s PIPE-FLO software www.engineered-software.com
Pipe absolute roughness
Pipe absolute roughness (e) tabulated are taken from from several sources. These values are for new pipes and typically for new design purpose. For aged pipes or debottlenecking purpose, higher roughness are expected.
Pipe absolute roughness (e) tabulated are taken from from several sources. These values are for new pipes and typically for new design purpose. For aged pipes or debottlenecking purpose, higher roughness are expected.
| Piping Material | Absolute roughness (Micron) | Source |
| drawn brass | 1.5 | (1,2) |
| drawn copper | 1.5 | (1,2) |
| commercial steel | 45 | (1,2) |
| wrought iron | 45 | (1,2) |
| asphalted cast iron | 120 | (1,2) |
| galvanized iron | 150 | (1,2) |
| cast iron | 260 | (1,2) |
| wood stave | 200 to 900 | (1,2) |
| concrete | 300 to 3000 | (1,2) |
| riveted steel | 900 to 9000 | (1,2) |
| Rubber (smooth) | 6 to 70 | (3) |
| Rubber (wire-reinforce) | 300 to 4000 | (3) |
| Stainless Steel / Titanium / Cu-Ni | 45.7 | (4) |
| Carbon steel (CS) non-corroded - General | 45.7 | (4) |
| Carbon steel (CS) non-corroded - Relief system | 150 | (4) |
| Carbon steel (CS) corroded | 457 | (4) |
| Fiberglass | 5 | (5) |
| PVC | 1.5 | (6) |
| Copper | 1.5 | (6) |
| Aluminum | 1.5 | (6) |
| RedBrass | 1.5 | (6) |
* 1m = 1,000 mm = 1,000,000 micron ; 1 mm = 1,000 micron
Pipe Relative roughness
Relative pipe roughness is the ratio of absolute roughness (e) by and pipe diameter (D) :
Relative Pipe Roughness = e/D
(1) Binder, R.C. (1973), Fluid Mechanics, Prentice-Hall, Inc. (Englewood Cliffs, NJ).
(2) GPSA & Crane Technical Paper No. 410M
(3) Darby, R. (2001), Fluid Mechanics for Chemical Engineers, Vol 2, Marcel Dekker, (NY)
(4) BP GP 44-80
(5) Fiberglass Pipe Handbook, SPI Composites Institute
(6) Enginereed Software’s PIPE-FLO software www.engineered-software.com
Thursday, October 9, 2008
What is event scheduler in HYSYS Dynamic simulation ?
What is event scheduler in HYSYS Dynamic simulation ?
The structure of event scheduler in HYSYS as follow :
Event scheduler is a useful tool for Dynamic simulation in HYSYS. It helps you to schedule your event in dynamic simulation. Dynamic simulation normally helps engineer to simulate different scenario (especially upset scenario) and testing functionality of control logic, etc.
For example, to simulate the start up of the plant, In the beginning, you need to open Valve-1, then 1 hr later, you need to close Valve-1, and start compressor and open Valve-2. These activities in sequence can be carried out manually when our integrator reaches our expected time. On the other hand, we may automate these activities using event scheduler in order to simplify work.
For example, to simulate the start up of the plant, In the beginning, you need to open Valve-1, then 1 hr later, you need to close Valve-1, and start compressor and open Valve-2. These activities in sequence can be carried out manually when our integrator reaches our expected time. On the other hand, we may automate these activities using event scheduler in order to simplify work.
The structure of event scheduler in HYSYS as follow :
Schedule-->Sequence--->Event--->Action
Action is final layer to help us to do our expected work, such as specify variable, set controller mode etc. You should also specify the condition to do the action, such as elapsed time or even logic.
Tuesday, October 7, 2008
Pyrophoric Fire
"Pyrophoric" material is any material can be ignited or burned spontaneously in air when it is scratched, or struck, cracked, etc.
Typical component is Sulfur in Carbon steel vessel. Ferum (Fe) in carbon steel vessel reacts with Sulfur present in fluid and formed iron sulfide (FeS) which is a pyrophoric material that oxidizes exothermically when exposed to air.
Refinery, LNG production and gas treatment plant may expose to sulfur. Iron sulfide scale may appeared in Carbon steel vessel. It is typically a conversion of iron oxide, Fe2O3 (rust) to iron sulfide (FeS) in an oxygen-free atmosphere where hydrogen sulfide gas is present.
In Oxygen-free environment (during normal operation) :
Fe2O3 + 3H2S ==> 2FeS + 3H2O + S
When expose to Oxygen (during maintenance) :
FeS + 3O2 ==> 2Fe2O3 + 4S + Heat
FeS + 7O2 ==> 2Fe2O3 + 4SO2 + Heat
Heat is dissipated quickly and white smoke of SO2 gas released and followed by pyrophoric fires. This process is quick and exothermic oxidation.
Typical component is Sulfur in Carbon steel vessel. Ferum (Fe) in carbon steel vessel reacts with Sulfur present in fluid and formed iron sulfide (FeS) which is a pyrophoric material that oxidizes exothermically when exposed to air.
Refinery, LNG production and gas treatment plant may expose to sulfur. Iron sulfide scale may appeared in Carbon steel vessel. It is typically a conversion of iron oxide, Fe2O3 (rust) to iron sulfide (FeS) in an oxygen-free atmosphere where hydrogen sulfide gas is present.
In Oxygen-free environment (during normal operation) :
Fe2O3 + 3H2S ==> 2FeS + 3H2O + S
When expose to Oxygen (during maintenance) :
FeS + 3O2 ==> 2Fe2O3 + 4S + Heat
FeS + 7O2 ==> 2Fe2O3 + 4SO2 + Heat
Heat is dissipated quickly and white smoke of SO2 gas released and followed by pyrophoric fires. This process is quick and exothermic oxidation.
Saturday, October 4, 2008
Wobbe Index
Wobbe Index (WI) is used to compare the combustion energy output of different composition fuel gases. Wobbe index is used to define interchangeability of fuel. Two fuels with identical Wobbe Index at given pressure and valve setting (orifice size), the energy output will be identical. The variation in WI is typically upto 5% (but maximum could be 10% for some manufacturer).
Wobbe Index (WI) is define as
WI = HHV / Sqrt (SG)
where
Sqrt = Square root of
HHV = High Heating Value (Btu/Scf)*
SG = Specific Gravity (MWgas / 28.96)
* Some may use Lower Heating Value to define WI
Other Interesting Article :
i) Conversion from Weight Fraction to Mole Fraction
ii)Unit Conversion in Energy in LNG Sector
Gas liquid Separator Sizing Using GPSA (11ed)
A gas liquid separator is used for bulk separation and mist eliminator i.e. vane type, mesh type, cyclone type) are used to promote liquid drop coalescence and separation from gas. Souder-Brown equation has been widely used in Oil and gas industry to size a gas liquid separator with and without mist eliminator.
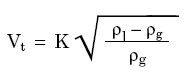
where
ρl = Liquid density, kg/m3 (or lb/ft3)
ρg = Vapor density, kg/m3 (or lb/ft3)
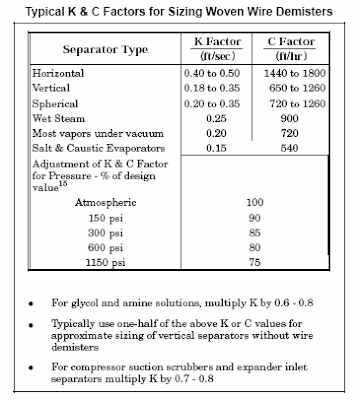
Generally the K factor as proposed in GPSA 11ed has been used by many engineers. Following figure tabulate the K factor may be used for horizontal, vertical, vertical scrubber and others separator for special services.
where
ρl = Liquid density, kg/m3 (or lb/ft3)
ρg = Vapor density, kg/m3 (or lb/ft3)
Generally the K factor as proposed in GPSA 11ed has been used by many engineers. Following figure tabulate the K factor may be used for horizontal, vertical, vertical scrubber and others separator for special services.

Wednesday, October 1, 2008
Why Droplet Still Fall at Terminal Velocity ?
Force balance Equation for terminal velocity of a freely falling droplet or particle
Force balance : Drag force + Buoyancy force = Gravity force
Lets take the case of freely falling droplet in a gas liquid separator, gas is flowing upwards and droplet is falling down now my, fundamental doubt is
A metal ball is held and once release in the air...
FORCE BALANCE
Drag force + Buoyancy force + External force + Gravity force = 0
Upward direction, Fd + Fb + Fe +(-Fg) = 0
==> Fd + Fb + Fe = Fg
Event at 0- second...
When the ball is at static condition (metal ball is held),
==> Fd is function of velocity and . As velocity is zero ==> Fd = 0
==> Fb is function of relative density between ambient and ball. Ball density (say metal ball is approx. 3000 kg/m3) relative to air (~1.3 kg/m3), it is almost negligible. ==> Fb=0
==> Thus, Fe= Fg, V=0 m/s
Event at 0+ second...
When the ball is just released (o+ second),
==> Fe = 0
==> Fb negligible. ==> Fb=0
==> Fg maintain with no change
==> Fd is function begin to increasing...
Net Force (Fg > Fd) will drive the ball downward. Ball velocity begin to increase.
Event at t second...
When the ball velocity increase upto terminal velocity (relative velocity between ball and gas),
==> Fe = 0
==> Fb negligible. ==> Fb=0
==> Fg maintain with no change
==> Fd increase upto terminal velocity
Terminal velocity
Ball velocity is increased upto a velocity where Fg = Fd, this velocity is called terminal velocity. At this velocity, net force = 0 as Fd = Fg ==> No further increase in velocity. Constant velocity.
Metal ball vs Droplet
Force balance : Drag force + Buoyancy force = Gravity force
- When all the force acting on the droplet get balanced (cancel out together), how the droplet can still fall ?
- Terminal velocity by definition is relative velocity of gas and droplet ?
A metal ball is held and once release in the air...
FORCE BALANCE
Drag force + Buoyancy force + External force + Gravity force = 0
Upward direction, Fd + Fb + Fe +(-Fg) = 0
==> Fd + Fb + Fe = Fg
Event at 0- second...
When the ball is at static condition (metal ball is held),
==> Fd is function of velocity and . As velocity is zero ==> Fd = 0
==> Fb is function of relative density between ambient and ball. Ball density (say metal ball is approx. 3000 kg/m3) relative to air (~1.3 kg/m3), it is almost negligible. ==> Fb=0
==> Thus, Fe= Fg, V=0 m/s
Event at 0+ second...
When the ball is just released (o+ second),
==> Fe = 0
==> Fb negligible. ==> Fb=0
==> Fg maintain with no change
==> Fd is function begin to increasing...
Net Force (Fg > Fd) will drive the ball downward. Ball velocity begin to increase.
Event at t second...
When the ball velocity increase upto terminal velocity (relative velocity between ball and gas),
==> Fe = 0
==> Fb negligible. ==> Fb=0
==> Fg maintain with no change
==> Fd increase upto terminal velocity
Terminal velocity
Ball velocity is increased upto a velocity where Fg = Fd, this velocity is called terminal velocity. At this velocity, net force = 0 as Fd = Fg ==> No further increase in velocity. Constant velocity.
Metal ball vs Droplet
Ball as compare to droplet, same principle applied. The differences area the droplet shape may change from time to time and drag coefficient (Cd) will change from time to time. From engineering perspective, the change (too small) is negligible.
Reference :
i) Gas liquid Separator Sizing Using GPSA
ii) Two Suction Nozzles on Drum for Two Pumps Operation...
Reference :
i) Gas liquid Separator Sizing Using GPSA
ii) Two Suction Nozzles on Drum for Two Pumps Operation...
Tuesday, September 30, 2008
How to Set Hot Pump Non-return Valve bypass Flowrate ?
Can someone suggest the flow rate through the Restriction Orifice (RO) on a pump warm-up bypass line for the standby pump, maybe a certain percentage of the rated flow of the running pump ?
Above question could be tackled in simple or difficult way. However lets start to understand the purpose, how it is implemented and how to set the flow.
Purpose
The main purpose of the bypass line is to maintain a minimum temperature different between the pump (and associate piping ) and the pump suction fluid temperature to avoid temperature shock in the event of standby pump is started-up automatically.
How it is implemented ?
The bypass can be a fixed RO, non-return valve with hole or a globe valve. It generally install across the standby pump discharge non-return valve.
How much flow ?
The bypass flow rate should be sufficient to cater for :
i) pump and associate piping heat-up from minimum ambient to normal suction temperature within a reasonable time i.e. 2 hours
ii) heat leakage via insulation during normal operation
Generally above calculation are time consuming.
Tips
Experience based approach may be taken where setting the RO / NRV hole size as 6-8 mm or install a one (1) in globe valve.
Reference :
i) Why bypass Non-Return Valve (NRV) ?
Above question could be tackled in simple or difficult way. However lets start to understand the purpose, how it is implemented and how to set the flow.
Purpose
The main purpose of the bypass line is to maintain a minimum temperature different between the pump (and associate piping ) and the pump suction fluid temperature to avoid temperature shock in the event of standby pump is started-up automatically.
How it is implemented ?
The bypass can be a fixed RO, non-return valve with hole or a globe valve. It generally install across the standby pump discharge non-return valve.
How much flow ?
The bypass flow rate should be sufficient to cater for :
i) pump and associate piping heat-up from minimum ambient to normal suction temperature within a reasonable time i.e. 2 hours
ii) heat leakage via insulation during normal operation
Generally above calculation are time consuming.
Tips
Experience based approach may be taken where setting the RO / NRV hole size as 6-8 mm or install a one (1) in globe valve.
Reference :
i) Why bypass Non-Return Valve (NRV) ?
Monday, September 29, 2008
Do i Normally Calculate Thermal Relief Load ?
Authority reserve the right to ask for calculation for thermal relief. If you or your company have done sufficient research and can be submitted to authority as supporting document, then don't waste your time to calculate it. Otherwise, you better get ready when authority ask for it...
In many event, a simple and smallest PSV i.e. DN 20 × DN 25 (NPS ¾ × NPS 1) would be sufficient for thermal relief.
Somehow if there is doubt the provided PSV is not adequate, it shall be calculated according to using Hydraulic expansion method may be used.
If the liquid being relieved potentially flash or form solids while it passes through the PSV, hydraulic expansion with two phase relief method may be used. Details refer to :
i) API Std 521 section 5.14.2., 5.14.3
ii) Thermal Relief of Non-Flashing Liquid in Pipe
iii) When Do i need a PSV for Thermal Relief on Piping ?
iv) Simple Flow Chart to Determine Requirement of Thermal Relief
In many event, a simple and smallest PSV i.e. DN 20 × DN 25 (NPS ¾ × NPS 1) would be sufficient for thermal relief.
Somehow if there is doubt the provided PSV is not adequate, it shall be calculated according to using Hydraulic expansion method may be used.
If the liquid being relieved potentially flash or form solids while it passes through the PSV, hydraulic expansion with two phase relief method may be used. Details refer to :
- J. C. LEUNG, "Size Safety Relief Valves for Flashing Liquids", Chemical Engineering Progress, February 1992, pp. 70-75
- J. C. LEUNG, and F. N. NAZARIO, "Two-Phase Flashing Flow Methods and Comparison", Journal of Loss Prevention Process Industries, Volume 3, Number 2, 1990, pp. 253-260
- L. L. SIMPSON, "Estimate Two-Phase Flow in Safety Devices", Chemical Engineering, August 1991, pp. 98-102
i) API Std 521 section 5.14.2., 5.14.3
ii) Thermal Relief of Non-Flashing Liquid in Pipe
iii) When Do i need a PSV for Thermal Relief on Piping ?
iv) Simple Flow Chart to Determine Requirement of Thermal Relief
When Do i need a PSV for Thermal Relief on Piping ?
Generally PSV not required for piping... however...API STD 521 2007 Addendum May 2008, section 5.14.1 (c) stated that hydraulic expansion due to solar heating on "long pipelines" shall be assessed and checked if a pressure relief valve (PSV) is required. What is "long pipelines" ? Difficult...
This section allows that a PSV may not required for thermal relief if proper administrative procedures and addition of signs stipulating the proper venting and draining procedures when shut-down and block-in are implemented. These action are acceptable and considered do not compromise the safety of personnel or equipment.
System under consideration for thermal relief consists of piping only (does not contain pressure vessels or heat exchangers), a pressure-relief device might not be required to protect piping from thermal expansion if :
- piping is always contains a pocket of non-condensing vapour, such that it can never become liquid-full (even it is heated and compressed); OR
- piping is in continuous use (i.e., not batch or semi-continuous use) and drained after being blocked-in using well supervised procedures or permits; OR
- fluid temperature is greater than the maximum temperature expected from solar heating (the pipe temperature direct under solar heating can reached approximately 60 °C to 70 °C, it can be as high as 85 °C for certain area i.e. Middle east) and there are no other heat sources such as heat tracing; OR
- the estimated pressure rise from thermal expansion is within the design limits of the equipment or piping.
Saturday, September 27, 2008
Conversion from Weight Fraction to Mole Fraction
A mixture consist of n component, e1, e2, e3,...en with molecular weight MW1, MW2, MW3, ... MWn. Each component mass are M1, M2, M3, ... Mn.
MASS FRACTION
Mass fraction of component-1, X1 = M1/MT [Eq. 1-1]
Mass fraction of component-2, X2 = M2/MT [Eq. 1-2]
Mass fraction of component-3, X3 = M3/MT [Eq. 1-3]
.
.
Mass fraction of component-i, Xi = Mi/MT [Eq. 1-i]
.
.
.
Mass fraction of component-n, Xn = Mn/MT [Eq. 1-n]
.
Total mass in mixtures, MT = M1 + M2 + M3 +...+ Mn [Eq. 2]
Number of MOLE
Component-1 number of mole, N1 = M1/MW1 [Eq. 3-1]
Component-2 number of mole, N2 = M2/MW2 [Eq. 3-2]
Component-3 number of mole, N3 = M3/MW3 [Eq. 3-3]
.
.
Component-n number of mole, Nn = Mn/MWn [Eq. 3-n]
Total number of mole,
NT = N1 + N2 + N3 +...+ Nn [Eq. 4]
NT = [M1/MW1 + M2/MW2 + M3/MW3 +...+ Mn/MWn] [Eq. 5]
MOLE FRACTION
For component-1,
Y1 = N1 / NT
Y1 = (M1/MW1) / NT
From [Eq. 1-1],
X1 = M1/MT
M1 = X1* MT
Y1 = (X1*MT/MW1) / NT
Mole Fraction of component-1,
Y1 = (M1/MW1) / NT [Eq. 6-1a]
Y1 = (X1*MT/MW1) / NT [Eq. 6-1b]
Mole Fraction of component-2,
Y2 = (M2/MW2) / NT [Eq. 6-2a]
Y2 = (X2*MT/MW2) / NT [Eq. 6-2b]
Mole Fraction of component-3,
Y3 = (M3/MW3) / NT [Eq. 6-3b]
Y3 = (X3*MT/MW3) / NT [Eq. 6-3b]
.
.
.
Mole Fraction of component-n,
Yn = (Mn/MWn) / NT [Eq. 6-na]
Yn = (Xn*MT/MWn) / NT [Eq. 6-nb]
Subscribe to:
Posts (Atom)